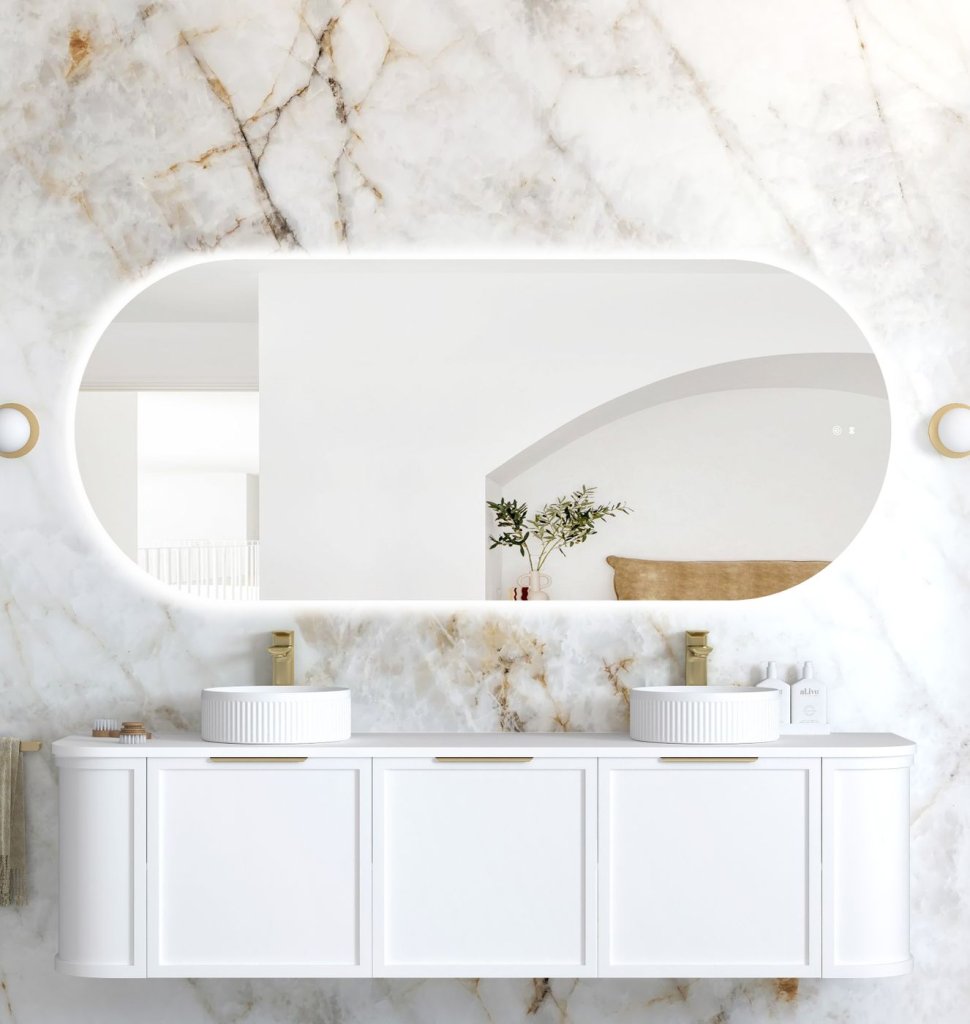
Hotel and commercial bathroom mirrors may appear to be straightforward products, but project procurement involves more than choosing a shape and placing an order. The mirror has to fit the wall build-up, coordinate with lighting and joinery, arrive without transit damage, and perform consistently across many rooms. If the model includes lighting, demisting, sensors or other electrical functions, the buyer also needs a clear record of the exact configuration being supplied.
A reliable procurement process turns design intent into measurable requirements before production begins. It also defines how samples will be approved, how changes will be controlled, what will be inspected, and what evidence will accompany the shipment. This guide provides a practical framework for hotel, apartment, workplace, retail and other commercial projects. Buyers can also review ArcQuay’s complete bathroom product catalog and mirror collection when preparing a project schedule.
1. Build a project brief that suppliers can manufacture against
The project brief should be specific enough to support costing, sampling, production and inspection. A mood board is useful for visual direction, but it is not a manufacturing specification. Consolidate the design team’s requirements into a controlled schedule with model references, drawings, quantities and room-type allocation.
Define the application and installation conditions
- Project and room type: identify guest rooms, public washrooms, accessible rooms, suites or other zones that may require different mirror sizes or functions.
- Mirror format: state whether the requirement is for a non-illuminated mirror, LED mirror, framed mirror, smart mirror or mirror cabinet.
- Wall and mounting conditions: provide the wall construction, finished surface, fixing zones, recesses, backing requirements and any restrictions on drilling.
- Interfaces: show clearances to basins, tapware, shelves, wall lights, power outlets, cabinetry and doors.
- Operating environment: describe expected humidity, cleaning regime, ventilation conditions and whether the installation is in a guest room or high-use public area.
Record dimensional and visual requirements
Issue dimensioned drawings rather than relying on nominal descriptions such as “large round mirror.” Record overall width, height or diameter, thickness, frame profile, corner radius, visible edge treatment, mounting position and permitted tolerances. For a framed model, define the approved finish with a physical sample or controlled color reference. For an illuminated model, document the desired lighting effect, color appearance, control method and any project-specific interface requirements.
The schedule should distinguish mandatory requirements from preferences. It should also state who has authority to approve substitutions. This prevents a visually similar but technically different component from entering production without review.
2. Use samples to close specification gaps
A sample is a decision tool, not just a sales presentation. The sample review should confirm proportions, reflection quality, edge finish, frame color, light distribution, controls, mounting method, service access and packaging. Install the sample in a representative wall condition where possible. A tabletop review may not reveal cable access problems, wall clearances or the way light interacts with surrounding finishes.
Comments should be consolidated into one approval record. Photograph the sample, identify its model and revision, list accepted deviations, and link it to the final drawing and bill of materials. If changes are required, decide whether photographs and documents are sufficient or whether a revised physical sample is necessary.
Once approved, the reference sample and its supporting documents become the comparison standard for production. The buyer and supplier should retain matching records. Any later change to glass, frame finish, driver, sensor, mounting hardware, packaging or another controlled component should follow written change approval rather than informal messaging.
3. Confirm compliance at model and destination level
Compliance should never be treated as a blanket brand statement. Requirements vary by destination, product construction, electrical features, installation method and the role of the importer or project specifier. A document applicable to one mirror family may not automatically cover another size, driver, control system or market variant.
For every model that requires evidence, request a document set that makes the relationship clear:
- the legal manufacturer or responsible applicant;
- the exact model numbers and variants included in the document scope;
- the referenced standard, scheme or regulatory basis;
- the issuing laboratory, certification body or authority, where applicable;
- issue dates, validity information and report or certificate identifiers;
- product labels, ratings, installation instructions and required warnings;
- the approved electrical components for illuminated or powered models.
Separate the checks for the mirror assembly, electrical equipment, wireless functions and destination-specific labeling when those subjects are relevant. The project team should verify acceptance with its local consultant, importer or authority before ordering. If the destination or configuration changes, review the evidence again. ArcQuay’s market information pages can help buyers frame regional questions, but final project acceptance must be based on the actual model and current local requirements.
4. Translate the approved sample into a production control plan
Before mass production, the supplier should work from a released drawing, approved bill of materials, finish reference, packaging specification and critical-to-quality checklist. A short pre-production review is valuable for confirming quantities by model, revision status, inspection stages, labeling, spare parts, documentation and the target shipment date.
Controls should follow the product risk. Incoming checks may cover mirror material, frames, electrical components, mounting hardware and printed materials. In-process checks can focus on dimensions, edge condition, frame assembly, wiring, functional operation and cleaning. Final checks should confirm that the finished product matches the approved reference and that the correct accessories and documents are packed with it.
Traceability does not need to be complicated, but it should be useful. Purchase order, model, production batch and carton information should allow the parties to identify the affected goods if a problem is discovered later. Photographs and inspection records should use the same model names as the commercial documents.
5. Agree an inspection and AQL philosophy before production
There is no single inspection percentage or acceptance rule that is appropriate for every mirror order. Lot size, product maturity, electrical content, project criticality, supplier history and the consequence of failure all influence the plan. The buyer and supplier should agree the sampling standard or project-specific method, inspection level, defect classes, acceptance and rejection numbers, and reinspection process before goods are presented for final release.
Defects are commonly grouped by consequence:
- Critical: a condition presenting an unacceptable safety risk or making the product unsuitable for release, such as unsafe electrical construction, dangerous sharp edges, insecure mounting components or broken glass.
- Major: a defect likely to prevent normal use or create a clearly unacceptable installation, such as incorrect dimensions, non-functioning lighting or demisting, wrong finish, missing hardware, significant visual distortion or a configuration that does not match the approved model.
- Minor: a limited cosmetic or workmanship issue that does not materially affect installation or normal operation but falls outside the agreed appearance standard.
These examples still need project-specific definitions, photographs and boundary samples. Some characteristics may warrant a higher inspection frequency or a 100% check even when the broader lot uses statistical sampling. The plan should state what happens after rejection: containment, sorting, corrective action, rework, replacement and reinspection should not be decided for the first time at the shipping deadline.
Practical final-inspection points
- model, quantity, dimensions, frame finish and revision match the order;
- reflective surface is clean and consistent with the approved sample under agreed viewing conditions;
- edges, corners, frame joints and visible surfaces meet the approved workmanship standard;
- mounting points, brackets, anchors and supplied hardware are correct for the documented system;
- lighting, controls, demisting and other specified functions operate correctly;
- cables, connectors, labels and component ratings match the approved configuration where applicable;
- instructions, care information and accessories are complete;
- carton identification matches the product and room or model schedule.
6. Validate packaging against the real distribution route
Mirror packaging should be designed around the product’s weak points and the shipment route. A single carton may pass through factory handling, container loading, sea or road transport, warehouses, pallet transfers and final delivery to a construction site. The protocol should therefore reflect the intended packed weight, carton size, pallet pattern and handling method rather than applying an arbitrary test copied from another product.
A useful packaging validation protocol includes the following steps:
- Approve the pack design. Record the carton grade, internal supports, edge and corner protection, surface films, accessory locations, moisture protection where specified, labels and pallet arrangement.
- Select representative samples. Use normal production components and include the heavier, larger or otherwise higher-risk models where the range varies.
- Document the starting condition. Photograph the product and packaging, record dimensions and gross weight, and complete a functional check before testing.
- Define the test sequence. Handling or drop events, vibration, compression, impact and other simulations should be selected and set by the agreed route risk or a recognized protocol when the contract requires one. Test levels must be written into the approved plan rather than assumed.
- Open and inspect. Check the glass, frame, backing, electrical functions, mounting kit, accessories and carton markings after the sequence. Look for damage as well as movement that could cause damage during a longer journey.
- Correct and retest. If the pack fails, document the cause, revise the design and repeat the relevant validation before shipment approval.
Transit testing is evidence for the tested configuration, not a guarantee for every size or logistics route. Any change to product weight, carton dimensions, internal supports, palletization or distribution method should trigger a review of whether revalidation is needed.
7. Plan replacements and spares as part of procurement
Replacement planning should start before the order is released. A blanket spare percentage can be either wasteful or inadequate, so the quantity should reflect model count, project location, installation schedule, product repairability, route risk and the time needed to reproduce a special finish.
Agree which items can be safely replaced on site and which require a complete unit. Depending on the approved design, the spare plan may include mounting hardware, approved drivers, sensors, control modules or complete mirrors. Each spare should be labeled to the same model and revision system as the installed product. Installation and replacement instructions must define work that requires a qualified trade or manufacturer support.
The commercial agreement should also describe the claim process: information required from site, photographs or test evidence, response contacts, disposition of damaged goods, compatibility confirmation and target decision times. Clear rules reduce delays when rooms are approaching handover.
8. Complete a controlled shipment handover
Shipment release is the point where product, quality and logistics records come together. Before loading, the buyer or its appointed inspector should receive an agreed handover pack. Depending on the order, it may include:
- commercial invoice and packing list with consistent model codes;
- carton quantities, gross and net weights, dimensions and pallet plan;
- batch or lot references and carton-label examples;
- final inspection report, photographs and disposition of any deviations;
- approved drawing, sample reference and bill-of-material revision;
- model-specific compliance documents requested for the destination;
- installation, operation, cleaning and maintenance instructions;
- spare-parts list and replacement contact process;
- loading photographs, seal information and shipping-document contacts.
Names should match across the schedule, inspection report, labels and shipping documents. Open deviations should be accepted in writing or resolved before release. For multi-phase projects, record lessons from the first shipment and update the next production or packaging plan through controlled revision.
A better mirror order begins before the purchase order
The strongest hotel and commercial mirror programs align design, manufacturing, inspection and logistics from the start. A precise brief reduces quotation assumptions. An installed sample reveals interface issues. Model-level evidence avoids broad compliance claims. A risk-based inspection plan and route-specific packaging protocol create objective release criteria. Replacement planning and a complete handover pack then support the site team after the container leaves the factory.
ArcQuay’s Project Solutions team can review mirror schedules alongside vanities and other bathroom products. To begin a model and project review, send the destination, quantities, drawings, required functions, target timeline and available compliance brief through the Get a Quote page. Recommendations and documentation can then be confirmed against the exact products proposed for your project.